Skip to content
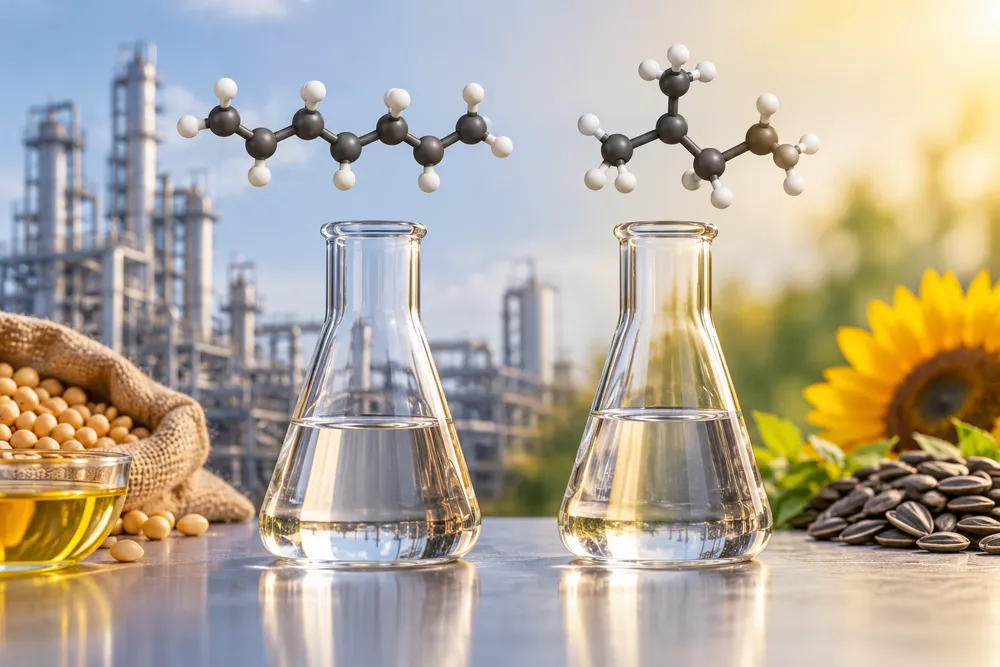
Few chemicals sit as quietly inside everyday life as cyclopentane. It is the leading physical blowing agent for the rigid polyurethane insulation that fills the walls of refrigerators and freezers, and it insulates the panels, pipes and cold-chain equipment that keep buildings efficient and food safe. Adopted after the Montreal Protocol eliminated ozone-depleting CFC-11 and HCFC-141b, this five-carbon ring hydrocarbon combines zero ozone-depletion potential with a global warming potential of only about 11. This article reviews its key properties, its dominant role in rigid PU foam, pentane blend strategies, plant safety practice, and the criteria that matter when selecting a cyclopentane supplier.
What Is Cyclopentane? Properties That Matter in PU Foam
Physical and chemical profile
Cyclopentane (CAS 287-92-3) is the smallest ring member of the cycloalkane family: five carbon atoms, each carrying two hydrogen atoms, giving the molecular formula C5H10 and a molecular weight of 70.13. At ambient temperature it is a colorless, mobile liquid with the familiar gasoline-like odor of light hydrocarbons. Its physical constants explain much of its industrial success. It boils at 49.3 °C, warm enough to remain an easily stored liquid yet cool enough to vaporize fully in the heat of a polyurethane reaction; it freezes only at −94 °C, so winter logistics pose no solidification risk; and its density of roughly 0.746 g/cm³ at 20 °C keeps volume-based metering simple. Like other hydrocarbons of similar size, it is practically insoluble in water.
- CAS number: 287-92-3 (UN 1146 for transport)
- Molecular formula: C5H10, a cycloalkane; molecular weight 70.13
- Boiling point: 49.3 °C
- Melting point: −94 °C
- Density: approximately 0.746 g/cm³ at 20 °C
- Appearance and odor: colorless transparent liquid, gasoline-like odor
- Water solubility: practically insoluble
The specification behind foam performance
Commercial material is normally offered in an industrial grade of 95% minimum purity and a foam grade of 99% or higher, with a narrow distillation range centered on the 49.3 °C boiling point. Water content deserves particular attention: water reacts with the isocyanate component of a PU system, generates extra carbon dioxide, and disturbs cell nucleation, so reliable producers hold it well below 0.01%. Even the impurity profile matters, because residual n-pentane and isopentane shift the vapor pressure inside the finished foam cells. Full analytical parameters and typical batch results are published on the cyclopentane product page of Dongying Eastchem.
Why the Foam Industry Replaced CFC-11 and HCFC-141b
The Montreal Protocol legacy
For decades, rigid polyurethane insulation depended on trichlorofluoromethane, better known as CFC-11. It was a chemically convenient blowing agent but an environmental catastrophe: with an ozone-depletion potential of 1.0, it served as the reference substance against which ozone damage is measured, and its elimination under the Montreal Protocol forced the foam industry to re-engineer insulation from first principles. The interim replacement, HCFC-141b, still attacked stratospheric ozone and was in turn scheduled out under the same treaty. Water-blown systems required no halogen at all, but the carbon dioxide they generate conducts heat too well for thin-walled, energy-labelled appliances, leaving manufacturers searching for a better answer.
F-gas rules closed the HFC detour
Hydrofluorocarbons such as HFC-245fa offered a zero-ODP bridge, but their global warming potentials reach several hundred times that of carbon dioxide, and the EU F-gas Regulation placed them under a strict phase-down. The five-membered ring emerged as the endgame: an ozone-depletion potential of zero, a GWP of only about 11 because its atmospheric lifetime is measured in days rather than decades, and a lower gas thermal conductivity than any practical HFC. Most of the world’s major appliance plants consequently standardized on hydrocarbon technology. Its environmental obligation is simply different in kind: as a volatile organic compound it is managed with capture and abatement equipment rather than greenhouse-gas accounting.
Cyclopentane as a Blowing Agent for Rigid PU Foam
In a rigid polyurethane formulation, the physical blowing agent does two jobs at once. It vaporizes in the heat of the exothermic polyol–isocyanate reaction, expanding the reacting mass into a fine-celled froth, and it then remains inside the closed cells, where its gas thermal conductivity largely determines the insulation value of the finished part. This molecule is unusually good at both: it boils at just the right moment in the temperature rise, and its relatively heavy, slow-diffusing molecules give the foam low initial conductivity together with long-term dimensional stability, because cell pressure declines slowly as small amounts diffuse out over the years.
Refrigerator and freezer insulation: the dominant application
Household refrigerators and freezers are where the cyclopentane blowing agent won its dominant position. Appliance foam must deliver demanding energy-label performance from ever-thinner cabinet walls, and hydrocarbon-blown foam reaches the design thermal conductivity that made it the default choice for the global appliance industry after the CFC phase-out. Chest freezers, display counters, beverage coolers and insulated shipping containers follow the same logic. For converters, the technology is mature: formulators and equipment suppliers have built deep process knowledge around this one blowing agent over more than two decades.
Panels, pipes and the wider insulated world
Beyond the kitchen, the same chemistry insulates the built environment and the cold chain:
- Insulated metal-faced sandwich panels for walls, roofs and cold rooms
- Pre-insulated pipe systems for district heating and cooling networks
- Refrigerated truck bodies, trailers and reefer containers
- Insulated garage and entrance doors, water heaters and vending cabinets
- Structural rigid foam parts where closed-cell content and stiffness matter
Beyond foam: solvents and reference fuels
The same low polarity and controlled evaporation profile support smaller-volume applications: as a reaction and extraction solvent, as an intermediate in organic synthesis, and as a component of reference fuels used in knock-testing of gasoline engines. These outlets reward exactly the tight distillation control that foam producers already demand.
Cyclopentane Blends: Balancing Conductivity, Flow and Flammability
Pure cyclopentane delivers the best insulation value in the pentane family, but it is not always the easiest agent to process. Its solubility in standard polyols is limited, blend viscosity climbs quickly, and froth flow in long, narrow mold cavities — a refrigerator cabinet is exactly that — can suffer before the foam fills every corner. Blending with a lighter pentane trades a small increase in gas thermal conductivity for better miscibility, lower viscosity and improved flow, and each blend family has found its niche:
- Neat systems, chosen where the lowest possible thermal conductivity justifies tighter process control
- Blends with isopentane, the appliance-industry compromise between insulation value and flow in long cabinet molds
- Blends with n-pentane, common in panel and boardstock production, where throughput and cost matter more than the last increment of lambda
- Water co-blowing, which trims hydrocarbon load while fine-tuning froth behavior and cell structure
Because blend performance depends on the quality of every component, many foam producers source n-pentane and isopentane from the same supplier to keep impurity profiles consistent from lot to lot. Pentane technology also reaches beyond polyurethane: expandable polystyrene (EPS) beads carry pentane as their expanding agent, and bead quality follows the same purity discipline that PU foam requires.
Safety in Pentane Foaming Plants: What Converters Must Get Right
A hazard profile that commands respect
Every pentane is highly flammable, and this one is no exception. Its flash point of −37 °C means the liquid can form an ignitable atmosphere at any temperature a factory will ever experience; its autoignition temperature of about 361 °C is within reach of hot surfaces and electrical equipment; and its vapors are heavier than air, traveling along floors and trenches toward distant ignition sources across a flammable range of roughly 1 to 9 percent by volume in air. These properties define its transport identity — UN 1146, Class 3 flammable liquid — and they define the engineering standard of any foaming plant that uses it.
Engineering controls that make hydrocarbon foaming routine
The industry solved hydrocarbon foam safety decades ago, and the required controls are well established:
- Hazardous-area classification with explosion-proof, ATEX-rated equipment throughout the foam line and premix room
- Nitrogen blanketing of storage tanks, day tanks and metering units to keep oxygen out of the vapor space
- Closed-loop, sealed premix and metering systems that eliminate open handling of the blowing agent
- Fixed gas detection with automatic interlocks, backed by high-rate ventilation wherever small releases are possible
- VOC capture and abatement, typically activated-carbon recovery, on exhaust streams
- Rigorous grounding and bonding, hot-work permits and static control during drum and tank transfers
How to Qualify a Cyclopentane Supplier
A refrigerator line pours cabinets around the clock, and a drifting blowing agent quickly shows up as thermal-conductivity drift, shrinkage or voids. Consistency therefore outranks almost everything else when buyers evaluate export sources. The checklist below reflects what appliance and panel formulators typically verify before a first trial shipment:
- Grade consistency: 99%-plus foam grade with distillation results, not just promises, on every certificate
- Water content held at the low levels that appliance systems require
- Batch-specific COA accompanying each shipment, with the impurity profile disclosed
- Dangerous-goods competence: ISO tanks, 200 L drums and tank trucks with complete UN 1146 documentation
- Responsive sampling and technical support for formulation questions
- Export experience with appliance-industry customers and their audit requirements
Dongying Eastchem Co., Ltd., a hydrocarbon specialist based in Dongying, Shandong, supports exactly this evaluation path: full specifications, packaging options and typical batch results are published on the cyclopentane product page, and every lot ships with its own certificate of analysis.
Conclusion: Partnering for Consistent Insulation Performance
This five-carbon ring earned its position as the world’s default insulation blowing agent by solving a regulatory problem without an engineering compromise: zero ozone-depletion potential, a GWP of only about 11, and gas thermal conductivity that keeps modern refrigerators and construction panels inside their energy budgets. Working with it successfully, however, is as much a supply question as a chemistry question — grades must be consistent, water content low and dangerous-goods logistics dependable from the producer’s tank farm to the converter’s premix room.
If you formulate appliance foam, panel stock or insulated pipe systems, Dongying Eastchem welcomes your inquiry. Visit the cyclopentane product page to review specifications and packaging, then contact the company through the website to request a certificate of analysis, discuss grade selection for your system, and obtain a current quotation for your volumes.