Skip to content
Why the n-/Iso-Pentane Blend Ratio Matters in EPS
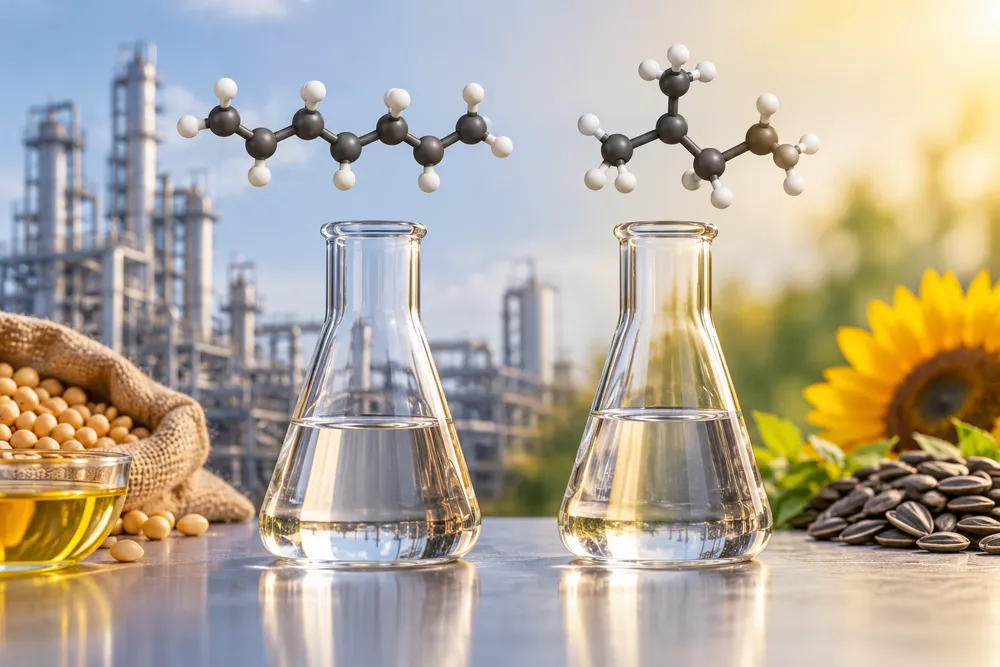
Expandable polystyrene (EPS) beads carry 4–7% pentane blowing agent locked into the polystyrene matrix. When steam hits the bead, that pentane vaporizes and inflates the polystyrene into foam. The blend between n-pentane (boiling point 36.1 ℃) and isopentane (boiling point 27.8 ℃) sets how fast the gas arrives — and through it, bead expansion speed, cell fineness, block density and fusion quality. Choosing and maintaining the right ratio for your process and season is one of the highest-leverage technical decisions in an EPS plant, and one of the cheapest to correct when a supplier can deliver both components and blends.
The Physics Behind the Ratio
Isopentane’s lower boiling point and higher vapor pressure mean it flashes earlier in the steam cycle: more expansion energy, delivered sooner. n-Pentane vaporizes later and more gently, continuing to inflate and fuse cells while the block is still under steam. A blend is therefore a timeline: the iso-fraction acts early, the n-fraction acts late. Too much iso and the bead can rupture or shrink back after demolding (gas leaves faster than the polymer can stabilize); too much n and pre-expansion becomes sluggish, densities climb and cycle times stretch. The same logic explains the seasonal rules below: summer workshops and cooling water are hot, so early gas release must be damped; winter everything is cold, so early energy must be boosted.
Recommended Ratios by Process and Season
Extrusion process (XPS board and direct extrusion): the ratio requirement is comparatively relaxed, because residence time and pressure in the extruder dominate gas retention. Common blends — N70/iso30, N60/iso40, N50/iso50 — all run acceptably, and many extruders fix one ratio year-round.
Suspension process (classic EPS bead): follow the season:
- Summer: n-/iso- 70/30 — the standard hot-season blend, damping early gas release to prevent collapse.
- Spring and autumn: transition blends around 50/50, switched when ambient temperatures cross roughly 20–25 ℃.
- Winter: n-/iso- 30/70 or 40/60 — extra fast iso-fraction supplies expansion energy against cold beads, cold water and cold molds.
These starting points assume standard block molding; thick blocks, very low target densities and high-steam systems all shift the optimum, typically by ±10% on the iso-share. The practical method is simple: record blend, steam profile, block density and shrinkage together, and let two weeks of data pick your plant’s exact numbers.
How the Blend Shows Up in Foam Quality
- Cell structure: higher iso-share tends toward finer early cells but higher rupture risk; higher n-share toward coarser, steadier cells.
- Block density: more iso helps reach low densities (15–20 kg/m3) at fixed cycle; more n raises density slightly but improves fusion.
- Shrinkage after demold: excessive iso or short aging causes blocks to shrink as residual gas diffuses out faster than air diffuses in — aging time and blend must move together.
- Fusion and surface quality: the late n-fraction pressure welds beads at the mold faces, reducing voids and improving cutting quality.
Quality Control: Measuring What You Actually Receive
Two tests protect a blending program. First, GC analysis of the delivered blend or of the two components — verifying the n/iso split within a few percent of order, plus purity 99%+ and low sulfur (sulfur poisons downstream catalytic uses and signals feedstock sloppiness). Second, residual-pentane monitoring of incoming EPS bead lots by headspace GC, so plant gas balance can be reconciled with the blend being fed. Suppliers who attach GC tracings to shipments make both tests routine instead of forensic.
Safety Essentials for Pentane Handling
Both pentanes are Class 3 flammables (UN 1265) with very low flash points (n-pentane −49 ℃, isopentane −51 ℃) and vapors heavier than air. Blending areas require explosion-proof equipment, grounding and bonding, vapor detection near floor level, and strict no-ignition discipline. Storage belongs in cool, ventilated, bunded solvent yards. These are manageable, standard solvent-plant requirements — but they are non-negotiable, and the SDS should be the working document in every shift.
Plant Practice: Blending, Storage and Steam Management
Plants that buy components rather than pre-mixed blends typically blend by mass in a dedicated, grounded, closed vessel: charge n-pentane, circulate, trim with isopentane to the target ratio, verify by GC or by calibrated density-refractive index check, and circulate again before feeding. Storage for both components belongs in bunded, ventilated solvent yards away from process buildings, with summer shading to limit vapor pressure growth. Feed lines to pre-expanders should be short, sloped and vapor-locked, because pentane vapor pockets cause inconsistent dosing — a subtle defect that masquerades as blend error. On the steam side, most ratio problems are actually steam problems: wet steam, fluctuating pressure or fouled jets change expansion more than a 5% blend drift does, so log steam conditions alongside blend data before adjusting chemistry.
Troubleshooting Guide: Five Defects and the Blend Response
- Beads collapse or shrink back during prefoaming: early gas release too strong — shift 5–10% toward n-pentane, lower prefoamer temperature, shorten residence.
- Blocks shrink after demolding: residual gas leaving faster than air enters — extend aging silo time and moderate the iso-share; verify bead residual pentane.
- Density cannot come down to target: insufficient early energy — raise iso-share or steam pressure; check that bead age is not too old (pentane loss with storage).
- Poor fusion, crumbly cut surfaces: late-stage pressure missing — raise n-share or extend final steam phase; check mold venting.
- Density varies block to block with identical settings: usually feed inconsistency or steam instability rather than blend — instrument before re-blending.
Seasonal Switch Management
Execute seasonal switches deliberately, not as an emergency: schedule the change two to three weeks ahead of the seasonal temperature crossover, run the first day at intermediate ratio, and hold density/shrinkage records through the transition. Most plants standardize two blends (summer 70/30, winter 40/60) and treat spring/autumn as scheduled transition windows with 50/50. Pre-mixed purchasing removes the labor but shifts discipline to order timing: two blend changeovers per year, ordered with enough lead time to run the old blend down before the new arrives — a coordination exercise EastChem supports with standing seasonal schedules.
Buying Blends vs Components: the Full Comparison
Pre-mixed blends remove a unit operation and a quality risk from your plant, arriving GC-verified and consistent — the right choice for operations without solvent-yard infrastructure or with lean technical staffing. Components buy flexibility: you tune ratios yourself for special block densities, react fast to unusual seasons, and typically price marginally better at scale — the right choice for plants with disciplined blending and laboratory control. A hybrid program captures both: standing blend deliveries for the seasonal standards, plus component stock for campaigns. Whichever model fits, the supplier requirement is identical — GC-verified lots, both components at 99%+ assay, and documentation that lets your records match the chemistry actually fed to your pre-expanders.
Supply Program from Dongying EastChem
We manufacture and supply both n-pentane (99%+) and isopentane (99%+) in 125 kg drums or ISO tanks, so plants can order pre-mixed seasonal blends or the two components for in-plant blending. Every lot carries a GC-backed COA. Consolidation is routine: pentanes ship with cyclopentane for PU insulation lines, styrene for EPS polymerization customers, and the full alkanes range. For deeper reading see our EPS polymer overview and the cyclopentane refrigeration articles on this site.
About this guide: the seasonal ratios above summarize field practice across suspension and extrusion EPS plants we supply. Your press, bead grade and climate set the final numbers — treat this page as the starting framework and let block records refine it. Blend guidance, seasonal windows and troubleshooting notes are updated as plant feedback accumulates, and our laboratory supports customers with residual-pentane and blend-ratio analysis during transitions. EPS producers planning capacity or seasonal programs can request the current supply schedule covering n-pentane, isopentane, cyclopentane and pre-mixed blends from one quality system. For engineering teams evaluating the switch from purchased blends to in-plant blending, or from one seasonal standard to a two-blend program, our staff reviews block records and proposes a transition plan with lab verification at each step, so the change happens between production campaigns rather than during one. Request the current blend calendar and pricing schedule with your next container inquiry; both documents arrive with the quotation and update automatically each season.
Frequently Asked Questions
Which blend ratio should I use for suspension EPS in summer?
Start at n-/iso-pentane 70/30. The higher share of slower n-pentane prevents premature gas release and bead collapse in hot workshops and warm cooling water.
And in winter?
Switch to n-/iso 30/70 or 40/60 so the fast isopentane fraction supplies expansion energy against cold beads, molds and water. Transition around 50/50 in spring and autumn.
Does the ratio matter as much for extrusion (XPS)?
No — extrusion systems tolerate roughly N70/30 to N50/50 year-round because residence time and pressure dominate. Many extruders fix one blend for the whole year.
Can you supply pre-mixed blends?
Yes. We deliver blends to your specified ratio with GC verification, or the two components separately for plants that blend in-house and switch seasonally.
My blocks shrink after demolding — is the blend wrong?
Possibly: high iso-share with short aging lets gas escape faster than air enters. Extend aging, or shift the blend 5–10% toward n-pentane, and track residual pentane in the bead.
What safety class are pentanes?
UN 1265 Class 3 flammable liquids with flash points near −50 ℃ and heavier-than-air vapor. Explosion-proof equipment, grounding and vapor discipline are mandatory; see the SDS.
Contact for quotations and samples:
Philip
WhatsApp / WeChat: +86 183 5460 9638
Email: [email protected]